FEEDWRIGHT
Feedwright CNC Calculator
Speeds and feeds, threads, tap drills, bolt circles, tapers, sine bar. Offline.
Free to try for 7 days, then unlock Pro once. No subscription.
Coming soon to Google Play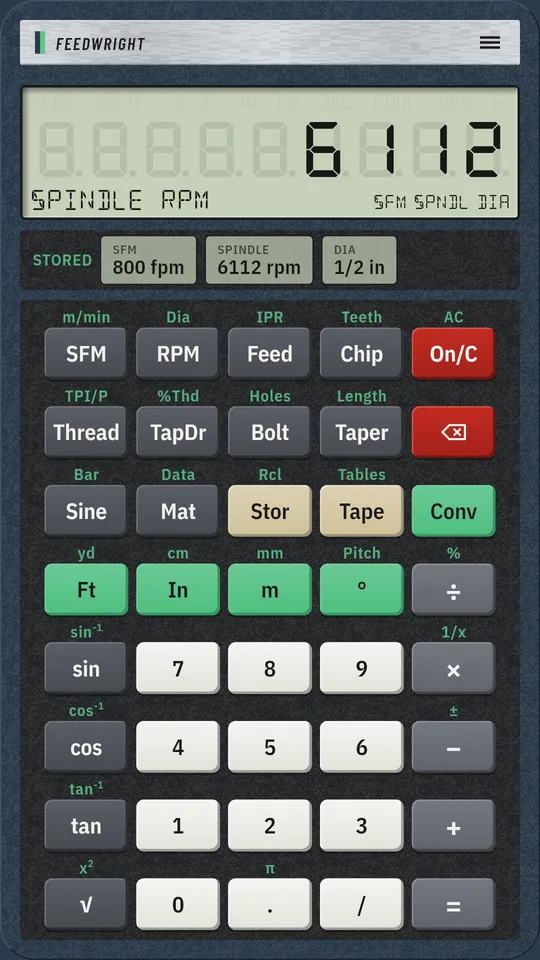
What it does
Feedwright is a shop calculator for machinists, CNC programmers and operators, toolmakers and students. It works like a hardware calculator: a steel-blue chassis, real keys and a clear LCD, with each answer labelled so you know what you are reading. Results are shown in decimals, the way machinists read them.
Speeds and feeds
- RPM from surface speed and diameter, in SFM or m/min
- Surface speed or diameter back from the other two
- Feed rate = RPM × chip load × number of teeth
- Feed per revolution, and feed from a feed per revolution
- Chip load per tooth from feed, RPM and teeth
Threads and tap drills
- Unified inch and ISO metric 60 degree threads
- Major, pitch and minor diameters and thread height
- Tap drill for 75 percent thread, or any percent you set
- Percent thread of a given drill
- Built-in tables of common unified and metric threads
Bolt circles
- X and Y of every hole from the centre, for any hole count
- Start angle for the first hole
- Chord distance between holes
Tapers and sine bar
- Included angle and compound setting from two diameters and a length
- Taper per foot and taper ratio
- The other diameter from a known angle
- Sine bar gauge block stack for an angle, or the angle for a stack, on a 5 in, 100 mm or any bar
Materials
- Starting surface speeds for high-speed steel and carbide in aluminium, mild steel, 4140, 304 stainless, cast iron, brass and titanium
- Brinell hardness from the indentation diameter, with a tensile strength estimate for steels
Works the way you do
- Inch and metric, and each thread keeps its own system
- A results strip shows every solved value at once
- 10 memories, a tape of your calculations, reference tables and a key guide
- Large keys you can hit with gloves on
Worked examples
- Spindle rpm. 800 SFM on a 1/2 in tool -> 6112 RPM.
- Feed rate. 6112 RPM, 0.002 in chip load, 4 flutes -> feed 48.9 in/min (then IPR).
- Tap drill. 1/4-20 at 75 percent thread -> tap drill 0.2013.
- Bolt circle. 6 holes on a 4.000 bolt circle -> hole 2 Y 1.7321.
- Taper. 1.000 to 0.750 over 3 in -> included angle 4.77 degrees.
- Metric rpm. Metric: 150 m/min on a 10 mm tool -> 4775 RPM.
How it's calculated
Every trade key and the formula behind it, as shown in the app's key guide. A second legend is the shifted function.
- SFM m/minSurface feet per minute / Cutting speed, metres per minute
- Stores the typed surface speed in feet per minute, or solves SFM = π × D × RPM ÷ 12; shifted works in metres per minute, Vc = π × D(mm) × RPM ÷ 1000.
- RPM DiaSpindle speed / Diameter
- Stores the typed spindle speed, or solves RPM = SFM × 12 ÷ (π × D) from the stored speed and diameter; shifted stores the tool or work diameter.
- Feed IPRFeed rate / Feed per revolution
- Stores the typed feed rate, or solves Feed = RPM × chip load × teeth; press again for feed per revolution. Shifted turns a typed feed per revolution into Feed = IPR × RPM.
- Chip TeethChip load per tooth / Number of teeth
- Stores the typed chip load per tooth, or solves chip load = Feed ÷ (RPM × teeth); shifted stores the flute count.
- Thread TPI/PThread / Threads per inch or pitch
- Stores the typed major diameter, or steps through it, pitch diameter D − 0.6495 × P, minor diameters and thread height; shifted stores threads per inch, or the pitch in mm for a metric thread.
- TapDr %ThdTap drill / Percent thread
- Tap drill = D − 1.299 × P × percent ÷ 100 for the stored thread; a typed drill size gives its percent thread instead. Shifted stores the percent thread, 75 by default.
- Bolt HolesBolt circle / Bolt holes
- Stores the typed bolt circle diameter, or steps through it, each hole's X and Y from the centre and the chord between holes; shifted stores the hole count, or a typed angle as the first hole's start angle.
- Taper LengthTaper / Taper length
- Type the large then the small diameter, pressing Taper after each; then gives the included angle 2 × atan((D − d) ÷ 2L), the compound setting, taper per foot and ratio. A typed angle gives the other diameter. Shifted stores the length.
- Sine BarSine bar / Sine bar length
- Gauge block stack = L × sin(angle) for the typed angle; a typed length gives the angle instead. Shifted stores the bar length, 5 inches or 100 mm by default.
- Mat DataMaterial / Material speeds and hardness
- Steps through workpiece materials; shifted shows starting surface speed ranges for high-speed steel and carbide (starting values only: adjust for machine and tool). A typed Brinell indentation in mm gives HB = 2F ÷ (πD(D − √(D² − d²))).
Results are computed from the formulas shown for each function and are provided for reference only. Material speeds are starting values: adjust for your machine, tooling, setup and coolant, and follow the tool maker's data. Verify every dimension before machining. The developer accepts no liability for loss or damage arising from use.
Get Feedwright
Free to try for 7 days, then unlock Pro once. No subscription. Works offline, no ads, no account.
Coming soon to Google PlayIn het Nederlands
Toerental, voeding, schroefdraad, tapboor, gatcirkel, conus en sinuslineaal.
Feedwright is een werkplaatsrekenmachine voor verspaners, CNC-programmeurs en -operators, gereedschapmakers en studenten. Hij werkt als een echte rekenmachine: een staalblauwe behuizing, echte toetsen en een helder LCD-scherm, met bij elk antwoord een label zodat u weet wat u leest. Resultaten verschijnen in decimalen, zoals verspaners ze lezen.
Gratis 7 dagen proberen, daarna eenmalig Pro ontgrendelen. Geen abonnement.