TACKWRIGHT
Tackwright Welding Calculator
Fillet and groove welds, weld weight, filler, heat input and CE. Offline.
Free to try for 7 days, then unlock Pro once. No subscription.
Coming soon to Google Play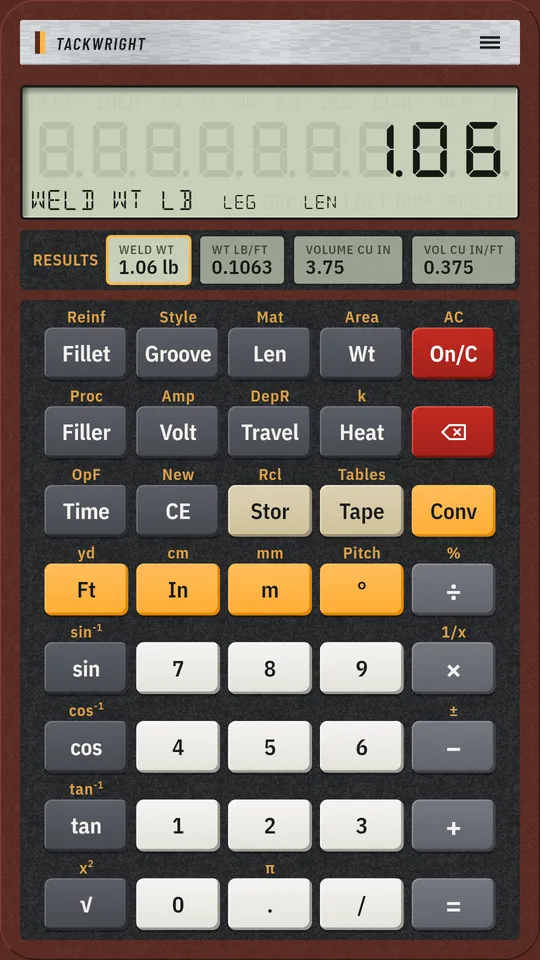
What it does
Tackwright is a welding calculator for welders, fabricators, welding inspectors, estimators and students. It works like a hardware calculator: an oxide-red chassis, real keys and a clear LCD, with each answer labelled so you know what you are reading.
Fillet and groove welds
- Fillet weld cross-section, throat (0.707 × leg) and face width from the leg size
- Convexity or reinforcement added to the cross-section
- Groove cross-section and face width for single V, single bevel, double V, double bevel and square grooves, from plate thickness, groove angle and root gap
Weld metal and filler
- Weld metal volume and weight, per foot or metre and in total
- Carbon steel, stainless or aluminium, or type any cross-section area
- Filler metal to buy from typical deposition efficiencies for SMAW, GMAW, FCAW, GTAW and SAW, or your own percentage
Heat input
- Heat input in kJ/in and kJ/mm from volts, amps and travel speed
- Q = k × arc energy, with ISO/TR 17671-1 thermal efficiency factors per process
- The travel speed for a target heat input
Arc time and labour
- Arc time from deposition rate or from travel speed
- Welder time at your operating factor
Carbon equivalent
- IIW carbon equivalent, typed element by element from the mill certificate
- Higher CE means more hardening risk: set preheat per the governing code
Works the way you do
- Inches or millimetres, fractions or decimals
- A results strip shows every solved value at once
- 10 memories, a tape of your calculations, reference tables (processes, densities, fillet sizes, CE) and a key guide
Worked examples
- Fillet weight. 1/4 in fillet, 10 ft, steel -> weld metal weight 1.06 lb.
- Heat input. 25 V, 200 A, 10 in/min -> heat input 30 kJ/in.
- Groove. 1/2 in plate single V, 1/8 in root gap -> V area 0.2068 sq in.
- Filler. 1/4 in fillet, 10 ft, SMAW at 60 % -> filler to buy 1.77 lb.
- Carbon equivalent. C 0.2, Mn 1, Cr+Mo+V 0.3, Ni+Cu 0.3 -> CE (IIW) 0.45.
- Metric heat input. 25 V, 200 A, 300 mm/min -> heat input 1 kJ/mm.
How it's calculated
Every trade key and the formula behind it, as shown in the app's key guide. A second legend is the shifted function.
- Fillet ReinfFillet weld / Reinforcement or convexity
- Stores the typed fillet leg size, or steps through it, the cross-section leg² ÷ 2 (plus 2/3 × face × convexity), the throat 0.707 × leg and the face width. Shifted stores the convexity or groove reinforcement height.
- Groove StyleGroove weld / Groove style
- Stores the typed plate thickness, or steps through it, the groove cross-section (single V: t² × tan(α/2) + gap × t), face width, angle and root gap. Shifted steps V, bevel, double V, double bevel and square; a typed angle sets the groove angle, a typed length the root gap.
- Len MatWeld length / Weld metal
- Stores the typed total weld length, or recalls it. Shifted steps through steel, stainless and aluminium for the weld metal density.
- Wt AreaWeld metal weight / Weld cross-section area
- Weld metal weight = area × length × density for the last fillet, groove or area typed; press again for weight per foot or metre, volume and area. A typed length is taken as the weld length. Shifted stores a typed cross-section area, or shows the area.
- Filler ProcFiller metal required / Welding process
- Filler metal to buy = weld metal ÷ deposition efficiency; press again for per foot or metre and the efficiency. Shifted steps SMAW, GMAW, FCAW, GTAW and SAW (typical efficiencies, low end); a typed percent sets your own efficiency.
- Volt AmpArc voltage / Welding current
- Stores the typed arc voltage; shifted stores the current.
- Travel DepRTravel speed / Deposition rate
- Stores the typed travel speed in inches or millimetres per minute. Shifted stores the deposition rate in pounds or kilograms per arc hour.
- Heat kHeat input / Thermal efficiency factor
- Heat input = V × A × 60 ÷ (1000 × travel speed) in kJ/in or kJ/mm; press again for the other unit and Q = k × arc energy. A typed heat input gives the travel speed for it. Shifted sets k, by default the process value from ISO/TR 17671-1.
- Time OpFArc time / Operating factor
- Arc time = weld metal ÷ deposition rate, or length ÷ travel speed; press again for the other and the welder time at the operating factor. A typed length is taken as the weld length. Shifted stores the operating factor in percent.
- CE NewCarbon equivalent / New steel
- Type C, Mn, Cr+Mo+V and Ni+Cu in percent, pressing CE after each; shows CE = C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15 (IIW). Higher CE means more hardening risk: set preheat per the governing code. Shifted starts a new steel.
For estimating and planning. Efficiencies and densities are typical values: check the filler maker's data. Verify every result against the welding procedure specification and the applicable code; it does not replace a qualified procedure or preheat requirement. The developer accepts no liability for loss or damage arising from use.
Get Tackwright
Free to try for 7 days, then unlock Pro once. No subscription. Works offline, no ads, no account.
Coming soon to Google PlayIn het Nederlands
Hoeklas en V-naad, lasgewicht, toevoegmateriaal, warmte-inbreng en CE. Offline.
Tackwright is een lasrekenmachine voor lassers, constructiebankwerkers, lasinspecteurs, calculators en studenten. Hij werkt als een echte rekenmachine: een roestrode behuizing, echte toetsen en een helder LCD-scherm, met bij elk antwoord een label zodat u weet wat u leest.
Gratis 7 dagen proberen, daarna eenmalig Pro ontgrendelen. Geen abonnement.